
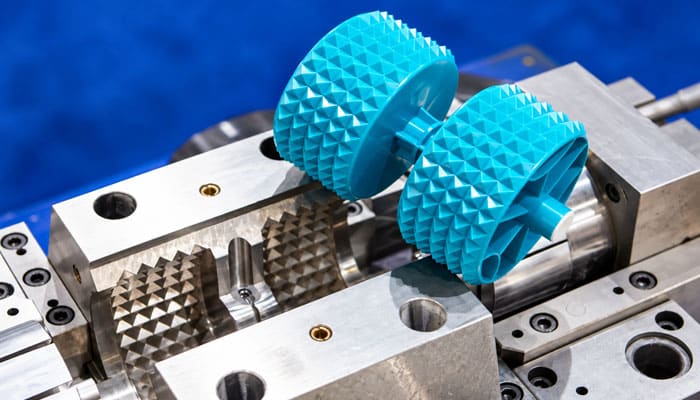

An injection-molded part can meet its initial dimensions and still fail early if the resin does not suit its application. Material choice affects load capacity, impact resistance, heat tolerance, chemical exposure, surface finish, and production consistency. It also influences shrinkage, warpage, cycle time, and part cost. A sound choice depends on service conditions and compares each demand with measurable material properties. The process requires companies to link each requirement to a testable performance measure.
A practical process for injection molding material selection starts with the part’s operating environment, rather than a preferred resin name. The designer should record expected loads, impact exposure, temperature range, chemical contact, electrical requirements, appearance goals, and production volume. This list gives material screening a clear basis and helps prevent changes after tooling or validation has begun.
Start With the Material Family
Thermoplastics and thermosets behave differently during molding and service. Thermoplastics soften when heated, so manufacturers can process them again without changing their chemical structure. Common examples include polyethylene, polypropylene, and polystyrene.
Thermosets cure through a chemical reaction that creates a permanent structure. After curing, they cannot be melted and reshaped. Epoxy and phenolic materials are perfect for applications that require heat resistance and dimensional stability, but their processing and recycling options differ from those of thermoplastics.
The material family sets the first boundary for design decisions. It affects processing temperature, recycling potential, part behavior, and the tooling and production controls the application requires.
Match Properties to Service Conditions
A load-bearing part needs sufficient tensile strength and stiffness. Impact resistance matters when the product faces drops, collisions, vibration, or sudden force. A resin selected only for stiffness can produce a part that handles steady loads but cracks during impact.
● Withstanding Heat and Thermal Stress
Temperature exposure requires separate review. A housing near a heat source needs a resin that retains its shape and mechanical properties at the operating temperature. Thermal cycling also matters because repeated heating and cooling can increase stress, distortion, or cracking.
- Evaluating Chemical Resistance
Chemical exposure can change material performance even when mechanical loads remain modest. Oils, solvents, cleaning agents, and moisture can cause swelling, embrittlement, discoloration, or surface damage. The resin should match the chemicals, concentration, contact time, and exposure temperature the product will encounter.
- Balancing Electrical and Visual Properties
Electrical products require review of dielectric strength and surface resistivity. These values help determine whether a resin provides the insulation or conductivity the design requires. Appearance also deserves early attention because color, gloss, transparency, and surface texture depend on the resin and the processing conditions.
Read Datasheet Values Correctly
Material datasheets provide test results, but those results need context. Tensile strength, elongation at break, modulus of elasticity, melting point, glass transition temperature, and thermal conductivity describe different aspects of performance.
- Comparing Test Methods
Test methods also affect comparisons. ASTM D638 measures tensile strength, while ASTM D3418 uses differential scanning calorimetry to determine melting behavior. A comparison is useful only when materials were tested under comparable methods and conditions.
- Understanding Filler Effects
Filler content can change the result. Glass-filled resins often provide greater stiffness and lower shrinkage, but they can increase tool wear and create directional properties. A part may behave differently along the flow direction than across it.
Datasheet values do not replace design validation. They provide a screening basis, while prototypes and functional tests confirm how the finished geometry behaves.
Consider Processing and Part Design
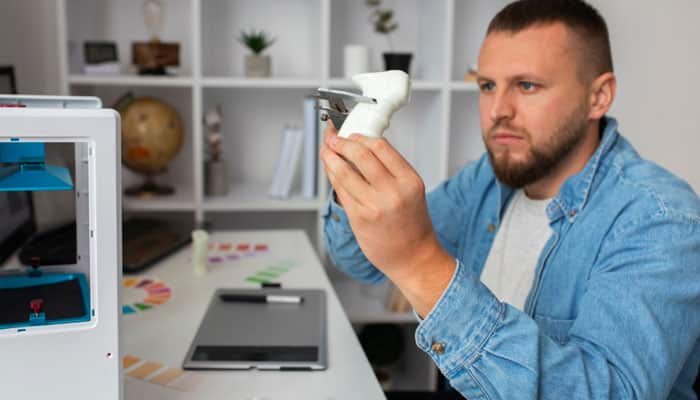
Material selection affects both molding conditions and service life. Resin viscosity influences how easily material fills thin walls, long flow paths, ribs, and other detailed areas. A resin that performs well in service can still create defects if the design exceeds its processing limits.
- Managing Dimensional Stability
Shrinkage and warpage require early review. Uneven wall thickness, abrupt thickness changes, and poor gate placement can produce distortion. Reinforced materials can reduce some forms of shrinkage while increasing differences along and across the flow direction.
- Controlling Resin Moisture
Moisture control also matters for hygroscopic materials. Moisture in the resin can cause surface defects, reduced strength, or hydrolytic degradation during molding. Drying requirements should appear in the process plan before production begins.
The material, mold design, and part geometry must be reviewed together. Changing the resin after tooling begins can affect gates, vents, cooling, draft, ejection, and dimensional targets.
Validate the Choice Before Production
A useful validation plan connects each material requirement with a measurable test.
- Drop testing checks impact behavior
- Load testing checks deformation or breakage under expected force
- Thermal cycling exposes changes caused by repeated temperature shifts
Chemical exposure tests should use the cleaning agents, oils, or solvents the product will encounter. Dimensional inspection should follow exposure when swelling or shrinkage could affect assembly.
Prototype testing also reveals processing issues that datasheets cannot predict. Short shots, sink marks, weld lines, flash, and warpage can indicate problems with material flow, mold temperature, cooling, or part design.
The final choice should document the resin grade, filler content, color, processing requirements, test results, and acceptance limits. This process prevents substitutions that change performance without formal review.
Conclusion
Material choice determines how an injection-molded part carries force, handles heat, resists chemicals, and maintains its dimensions over time. The best decision links service conditions to datasheet properties, then confirms those links through prototypes and functional testing.
Before approving a resin, the design team should create a requirement matrix, identify the governing properties, and test the highest-risk failure modes. This step reduces late tooling changes and gives product life a measurable foundation.
